T-Drill Raw Material Requirements
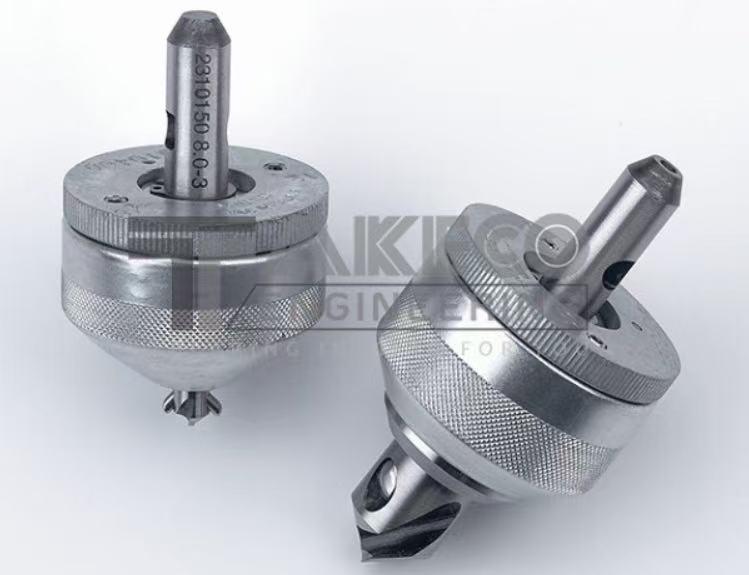
The T-Drill chipless forming process is widely used in heat exchanger manufacturing to create branch connections on main tubes without cutting chips. Its stable forming quality relies heavily on strict raw material control. Unsuitable tube materials will lead to cracking, wrinkling, uneven collar height and poor dimensional consistency, so clear raw material standards must be followed before production.
First, material ductility is the core requirement. The T-Drill process belongs to cold plastic deformation, so only malleable metals are applicable. Common qualified materials include copper, brass, aluminium, mild carbon steel and austenitic stainless steel. These materials have good elongation and can withstand local stretching and flanging during the collaring operation. Brittle materials with low elongation, such as high-hardness martensitic stainless steel and cast alloys, are not recommended, as they tend to crack at the hole edge under cold forming force.
Second, chemical composition and material purity need tight control. Impurity elements like sulfur and phosphorus should be kept at low levels. Excessive impurities will form internal inclusions, which become crack sources during deformation. For copper tubes used in HVAC and refrigeration, oxygen content must be controlled; deoxidized copper is preferred to avoid microcracks. Each batch of raw tubes should come with material test certificates, verifying chemical composition, tensile strength and elongation.
Third, tube dimensional accuracy and surface condition are critical. The outer diameter, wall thickness and straightness must meet tolerance specifications. Uneven wall thickness will cause asymmetric deformation and inconsistent collar size. The tube surface should be free of scratches, oxide scale, oil stains and dents. Surface defects expand rapidly under local stretching, resulting in rejected parts. Seamless tubes are generally preferred, while welded tubes require reliable weld quality and uniform weld reinforcement.
Finally, material hardness and metallurgical structure must be consistent. Over-hard material increases forming load and shortens tool life; over-soft material easily causes excessive thinning and wrinkling. Annealed or soft-temper states are usually selected for T-Drill processing. Uniform grain structure helps achieve repeatable forming results. If raw material hardness fluctuates widely between batches, machine parameters need frequent adjustment, lowering production efficiency and stability.
In conclusion, the T-Drill process demands raw materials with good ductility, stable chemical composition, precise dimensions, clean surfaces and uniform hardness. Standardized incoming inspection is essential to guarantee high-quality collar forming and long-term tool performance.

 English
 Arabic
 French
 Spanish
 Portuguese
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek