


Industrial Conveyors: Improving Manufacturing Efficiency with Advanced Material Handling Solutions
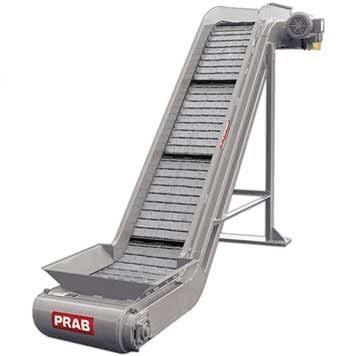
Modern manufacturing facilities depend on efficient material handling systems to maintain productivity, reduce operational costs, and improve workplace safety. Industrial conveyors play an essential role in moving materials, metal scraps, chips, and finished components throughout production facilities. From CNC machining and metal stamping to die casting and forging, reliable conveyor systems help businesses streamline operations and maintain consistent production workflows. Visit: Scrap Conveyor
PRAB provides a comprehensive range of industrial conveyor solutions designed to handle demanding manufacturing environments. Its metal scrap conveyor systems are engineered to transport different types of materials while supporting efficient scrap management, recycling, and production processes.
The Importance of Industrial Conveyor Systems
Industrial conveyors help manufacturers automate material transportation and reduce the need for manual handling. In metalworking facilities, machining operations generate metal chips, turnings, swarf, and other scrap materials that must be removed regularly. Without an effective transportation system, accumulated scrap can interrupt production, create workplace hazards, and increase maintenance requirements.
Automated conveyor systems provide a practical solution by continuously moving waste materials away from machines and transferring them to collection, processing, or recycling equipment. This improves production efficiency, supports cleaner working environments, and allows employees to concentrate on essential manufacturing activities.
Different Types of Industrial Conveyors
Selecting the appropriate conveyor depends on the material being transported, production volume, moisture levels, and facility layout. PRAB offers several conveyor technologies designed for different industrial applications.
Steel Belt Conveyors: These heavy-duty systems are suitable for transporting wet or dry metal scrap, including stamping waste, turnings, and machining chips. Their durable construction makes them appropriate for demanding manufacturing operations.
Pivot Belt Conveyors: Designed for oily and thin-gauge scrap, these conveyors help prevent materials from sticking to the belt. They are particularly useful in metal stamping applications where consistent scrap transportation is important.
Oscillating Conveyors: These systems use controlled movement to transport hot, wet, or abrasive metal chips. They are suitable for applications requiring reliable horizontal material transfer. Checkout: Metal Scrap Conveyors
Magnetic Conveyors: Magnetic technology allows these systems to transport ferrous metal chips, turnings, and stamping scrap while minimizing material carryover.
Drag Conveyors: Built for challenging industrial environments, drag conveyors handle highly abrasive materials and heavy metal scrap. Their robust construction supports demanding production requirements.
Pneumatic Conveyors: These systems use air movement to transport wet or dry metal chips across manufacturing facilities. They offer flexible routing options when conventional floor-level transportation is unsuitable.
Benefits of Automated Conveyor Solutions
Investing in an appropriate industrial conveyor system can deliver several operational advantages.
First, automation reduces manual material transportation and improves production efficiency. Workers spend less time handling scrap, while manufacturing equipment can operate with fewer interruptions.
Second, conveyor systems contribute to workplace safety. Removing accumulated metal waste helps reduce floor obstructions, potential slip hazards, and unnecessary forklift movement.
Third, durable industrial conveyors can lower maintenance expenses over time. Heavy-duty components and application-specific engineering help equipment withstand abrasive materials, demanding temperatures, and continuous production schedules.
Another important advantage is improved resource recovery. When conveyors are integrated with metal chip processing equipment, manufacturers can transfer scrap directly to crushers, wringers, centrifuges, and briquetting systems. These technologies help separate valuable metal materials from cutting fluids, supporting recycling and reducing waste.
Applications Across Manufacturing Industries
Industrial conveyor systems are used in numerous manufacturing environments. In CNC machining facilities, they remove metal chips and turnings generated during cutting operations. In die-casting plants, specialized conveyors transport hot metal scrap and components safely.
Metal stamping operations benefit from automated systems that collect and transfer scrap from presses to designated processing areas. Forging facilities require equipment capable of handling heavy materials and elevated temperatures.
Scrap yards and metal recycling facilities also depend on reliable conveyor systems to move large quantities of material efficiently. Choosing equipment designed for the specific application helps maintain consistent performance across different production environments.
Choosing the Right Conveyor System
Before investing in industrial conveyors, manufacturers should evaluate several important factors. These include the type and size of materials, scrap weight, moisture content, operating temperature, transportation distance, and required processing capacity.
Facility layout is equally important because some applications require straight conveyors, while others need inclined, L-shaped, Z-shaped, or in-floor configurations. Understanding these requirements helps businesses select equipment that integrates smoothly with existing production machinery.
Working with experienced conveyor engineers can also simplify equipment selection. Application assessments and material testing help determine suitable conveyor configurations and performance requirements before installation.
Why Consider PRAB Conveyor Solutions?
PRAB specializes in industrial material handling, metal scrap processing, and fluid recycling equipment. Its conveyor portfolio includes multiple technologies designed for machining, stamping, die casting, forging, and other demanding manufacturing applications.
The company also focuses on integrating conveyors with downstream processing and coolant recycling systems. This approach allows manufacturers to create more efficient material management operations while recovering valuable resources. Visit here: Metal Scrap Conveying Systems
With application-specific engineering, performance verification, maintenance programs, and technical support, PRAB helps manufacturers develop reliable material handling solutions.
Conclusion
Industrial conveyors are essential for improving productivity, workplace safety, and material handling efficiency in modern manufacturing facilities. Selecting the right system can reduce manual handling, minimize production interruptions, and support more effective scrap recycling.
With its extensive range of metal scrap conveyors and integrated processing technologies, PRAB offers manufacturers practical solutions for managing challenging industrial material handling requirements. Investing in properly engineered conveyor equipment can help businesses build more efficient, reliable, and sustainable manufacturing operations.
For more information visit our website: https://www.prab.com/conveyors/

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Greek
